- Home
- Blog
- Sure! Please provide the original title or the news content related to "Water Adhesive" so I can help rewrite the SEO title for you.
Sure! Please provide the original title or the news content related to "Water Adhesive" so I can help rewrite the SEO title for you.
By:Admin
Company News & Blog
Discover the Benefits of Waterborne Acrylic Resin for Your Next Project
Waterborne Acrylic Resin is a revolutionary product that is changing the game in the coatings industry. This environmentally friendly resin provides excellent performance and incredible versatility, making it a top choice for a wide range of applications. With its low volatile organic compound (VOC) content and ease of use, Waterborne Acrylic Resin is leading the way towards a more sustainable future.One company that is at the forefront of this innovation is {}, a leading manufacturer and supplier of specialty chemicals and materials. With a strong commitment to research and development, {} has been instrumental in the development and commercialization of Waterborne Acrylic Resin, and is dedicated to providing customers with high-quality, eco-friendly solutions.Waterborne Acrylic Resin offers a multitude of benefits for both manufacturers and consumers. Its low VOC content makes it an ideal choice for environmentally conscious companies looking to reduce their carbon footprint and meet strict environmental regulations. Additionally, its water-based formula makes it easy to clean up, reducing the need for harsh solvents and simplifying the overall coating process.One of the key advantages of Waterborne Acrylic Resin is its exceptional performance characteristics. It offers outstanding weathering and durability, making it suitable for a variety of interior and exterior applications. Whether used in architectural coatings, automotive finishes, or industrial coatings, Waterborne Acrylic Resin delivers superior adhesion, flexibility, and resistance to chemicals and abrasion.Beyond its performance, Waterborne Acrylic Resin also offers excellent versatility. It can be formulated to achieve a range of finishes, from high-gloss to matte, and can be tinted to create custom colors. This flexibility allows manufacturers to customize their coatings to meet specific customer requirements, expanding the possibilities for creative and innovative products.In addition to its environmental and performance benefits, Waterborne Acrylic Resin also offers economic advantages. Its ease of use and compatibility with existing application equipment help reduce production costs and increase efficiency. Furthermore, its fast drying time and low odor make it an attractive option for applications where minimal downtime and minimal disruption are critical.As a leading manufacturer and supplier of Waterborne Acrylic Resin, {} is committed to providing customers with top-notch technical support and customer service. With a team of experts dedicated to helping customers optimize their formulations and achieve the best results, {} sets itself apart as a trusted partner in the coatings industry.Furthermore, {} has made significant investments in its production facilities and supply chain to ensure a reliable and consistent supply of Waterborne Acrylic Resin to meet the growing demand of customers worldwide. This dedication to excellence has earned {} a reputation for delivering high-quality, sustainable products that exceed customer expectations.In conclusion, Waterborne Acrylic Resin is a game-changing innovation that is revolutionizing the coatings industry. Its environmental friendliness, exceptional performance, versatility, and economic advantages make it a top choice for manufacturers and consumers alike. With a commitment to excellence and a dedication to sustainability, {} is leading the way in providing customers with high-quality solutions for a more sustainable future.
Discover the Versatile Uses of Polyurethane in Various Industries
Polyurethane Application Offers Diverse Solutions for Various IndustriesPolyurethane is a versatile material that is widely used in various industries due to its unique properties and applications. From construction and automotive to furniture and packaging, polyurethane has become an essential material in manufacturing, providing countless benefits and solutions for different needs.One company at the forefront of innovative polyurethane applications is {Company Name}. With over 20 years of experience in the industry, they have been providing high-quality polyurethane products and solutions to a wide range of clients, offering tailored solutions to meet specific requirements.One of the key areas where {Company Name} excels is in the construction industry. Their polyurethane products are used in insulation, roofing, sealants, and adhesives, providing excellent thermal insulation and waterproofing properties. This not only helps in reducing energy costs but also contributes to sustainable and eco-friendly construction practices.In the automotive industry, {Company Name} provides polyurethane foam for vehicle interiors, seating, and acoustic insulation, offering enhanced comfort, durability, and noise reduction. Their expertise in developing custom solutions has made them a trusted partner for many automotive manufacturers, ensuring high-quality and reliable products for their vehicles.Moreover, the furniture and bedding industry also benefit from {Company Name}'s polyurethane applications, as they offer foam solutions for mattresses, upholstery, and comfort cushions. Their foam products are known for their resilience, support, and comfort, making them a preferred choice for customers seeking high-performance furniture and bedding materials.Another important sector where {Company Name} has made a significant impact is in the packaging industry. Their polyurethane foam packaging provides superior protection for fragile and sensitive products during shipping and handling, ensuring that items reach their destination intact and undamaged.In addition to these industries, {Company Name} also caters to the medical, sports, and leisure sectors, offering specialized polyurethane solutions for prosthetics, sports equipment, and recreational products. Their commitment to innovation and continuous improvement has led to the development of advanced materials that enhance performance and functionality across various applications.Beyond their diverse product offerings, {Company Name} is dedicated to sustainability and environmental responsibility in their manufacturing processes. They have implemented measures to reduce waste, minimize energy consumption, and optimize resources, aiming to create a greener and more sustainable future for the industry and society as a whole.Furthermore, {Company Name} places a strong emphasis on research and development, constantly seeking new ways to improve their products and create innovative solutions for their customers. Their team of experts and engineers work closely with clients to understand their specific needs and provide tailored polyurethane applications that meet and exceed expectations.The company's commitment to quality and customer satisfaction has earned them a reputation for excellence in the industry. Their focus on delivering reliable and high-performance polyurethane products has led to long-standing partnerships with clients worldwide, who trust {Company Name} to provide them with the best solutions for their needs.In conclusion, {Company Name} has established itself as a leading provider of polyurethane applications, offering diverse solutions for a wide range of industries. Their dedication to innovation, quality, and sustainability sets them apart in the market, making them a trusted partner for businesses seeking high-quality polyurethane products and customized solutions. As they continue to expand their capabilities and push the boundaries of what polyurethane can achieve, {Company Name} is poised to remain at the forefront of the industry for years to come.
Water-Based Urethane for Wood and Concrete Floors: A Comprehensive Guide
When it comes to choosing the right floor finish, there are several options to consider. One of the most popular choices is water-based urethane floor finish. This type of finish offers many benefits over traditional oil-based finishes, making it a top choice for homeowners and business owners alike.Water-based urethane floor finish is an environmentally-friendly option that is easy to use and maintain. It is made from a blend of synthetic resins that provide a durable, long-lasting finish that is resistant to abrasions, scratches, and water damage. This type of finish is perfect for high-traffic areas like living rooms, kitchens, and offices, where spills and scratches are more likely to occur.One of the primary benefits of water-based urethane floor finish is its low VOC content. Volatile organic compounds, or VOCs, are air pollutants that can have harmful effects on your health. Because water-based urethane floor finish contains fewer VOCs than oil-based finishes, it is a safer and healthier choice for your family or employees.Another advantage of water-based urethane floor finish is its reduced drying time. Unlike oil-based finishes, which can take up to 24 hours to dry, water-based urethane floor finish dries in just a few hours, allowing you to complete your project faster. This means you can walk on your newly finished floors much sooner than with oil-based finishes.Water-based urethane floor finish is also easier to clean and maintain. Because it is water-based, you can clean it with just soap and water, without having to use harsh chemicals that can damage the finish. Additionally, the durable nature of this finish means that you won’t have to refinish your floors as often, saving you time and money in the long run.When it comes to applying water-based urethane floor finish, there are two primary methods: spraying and rolling. Spraying is the preferred method for large areas like gymnasiums, while rolling is preferred for smaller areas like bedrooms. Regardless of the method you choose, be sure to follow the manufacturer's instructions carefully and use the appropriate safety equipment, such as gloves and a respiratory mask.In conclusion, water-based urethane floor finish is an excellent option for anyone looking to protect and enhance the look of their floors. It offers a range of benefits over traditional oil-based finishes, including reduced VOC content, shorter drying time, and easier maintenance. So if you're in the market for a durable, easy-to-use floor finish, consider water-based urethane floor finish.
Can Water Based Polyurethane be Applied Over Latex Paint?
story about water-based polyurethane and polycrylic in home improvement.As the world becomes more conscious of the environment, homeowners are opting for water-based products that are eco-friendly and safe to use. Water-based polyurethane and polycrylic are two such products that have gained popularity in the home improvement industry. They are easy to use, durable, and available at most hardware stores.Water-based products are gaining popularity over oil-based products because of their eco-friendliness. Water-based polyurethane and polycrylic have lower levels of volatile organic compounds (VOCs), which are harmful chemicals that can evaporate and cause health problems when inhaled. These products also have a lower odor, which makes them ideal for indoor projects.Water-based polyurethane is a protective coating used for finishing wood floors, cabinets, furniture, and other wooden surfaces. The product is easy to apply and dries quickly, making it a popular choice for DIY enthusiasts. The product is available in various finishes, including gloss, satin, and matte. Water-based polyurethane provides a durable finish that is resistant to scratches, scuffs, and stains. It also enhances the natural beauty of wood grain.Polycrylic is another water-based protective coating used for finishing wood surfaces. It is popular for its ease of use and fast drying time. Polycrylic is ideal for beginners and homeowners who want a quick and durable finish. The product is available in clear and tinted finishes, which can enhance the natural color of wood. It can also protect painted surfaces from fading, yellowing, and chipping.Both water-based polyurethane and polycrylic can be used on top of latex paint, as long as the paint has completely dried. The cure time for latex paint can vary from two hours to 30 days, depending on the brand and type of paint. It is important to follow the manufacturer's instructions for curing time and application.Water-based polyurethane and polycrylic should be applied with a foam brush, synthetic bristle brush, or a spray gun. It is important to avoid over-brushing, which can cause bubbles or streaks in the finish. The products should be applied in thin, even coats and allowed to dry completely between each coat. The number of coats will depend on the desired finish and level of protection needed.The water-based polyurethane and polycrylic products are available at most hardware stores, including Home Depot, Lowe's, and Ace Hardware. These products are manufactured by several companies, including {insert brand names}, who are leading the way in creating eco-friendly finishing products. These companies prioritize consumer health and environmental safety, ensuring their products meet or exceed industry standards.In conclusion, water-based polyurethane and polycrylic are popular choices for homeowners who want an eco-friendly, durable, and easy-to-use protective coating for their wooden surfaces. With the increase in environmental awareness, these products are gaining popularity over their oil-based counterparts. They offer a range of finishes and protection levels, making them suitable for various DIY projects. With the right application technique and curing time, homeowners can achieve a professional-looking finish that protects and enriches the natural beauty of wood.
High-Quality PU Based Paint for Durable Coatings
Certainly! Please provide the news content and the company introduction you'd like me to use for writing the 800-word news article.
Global DMPA Market Projected to Reach $974.5 Million by 2033, Growing at 6.4% CAGR: Future Market Insights
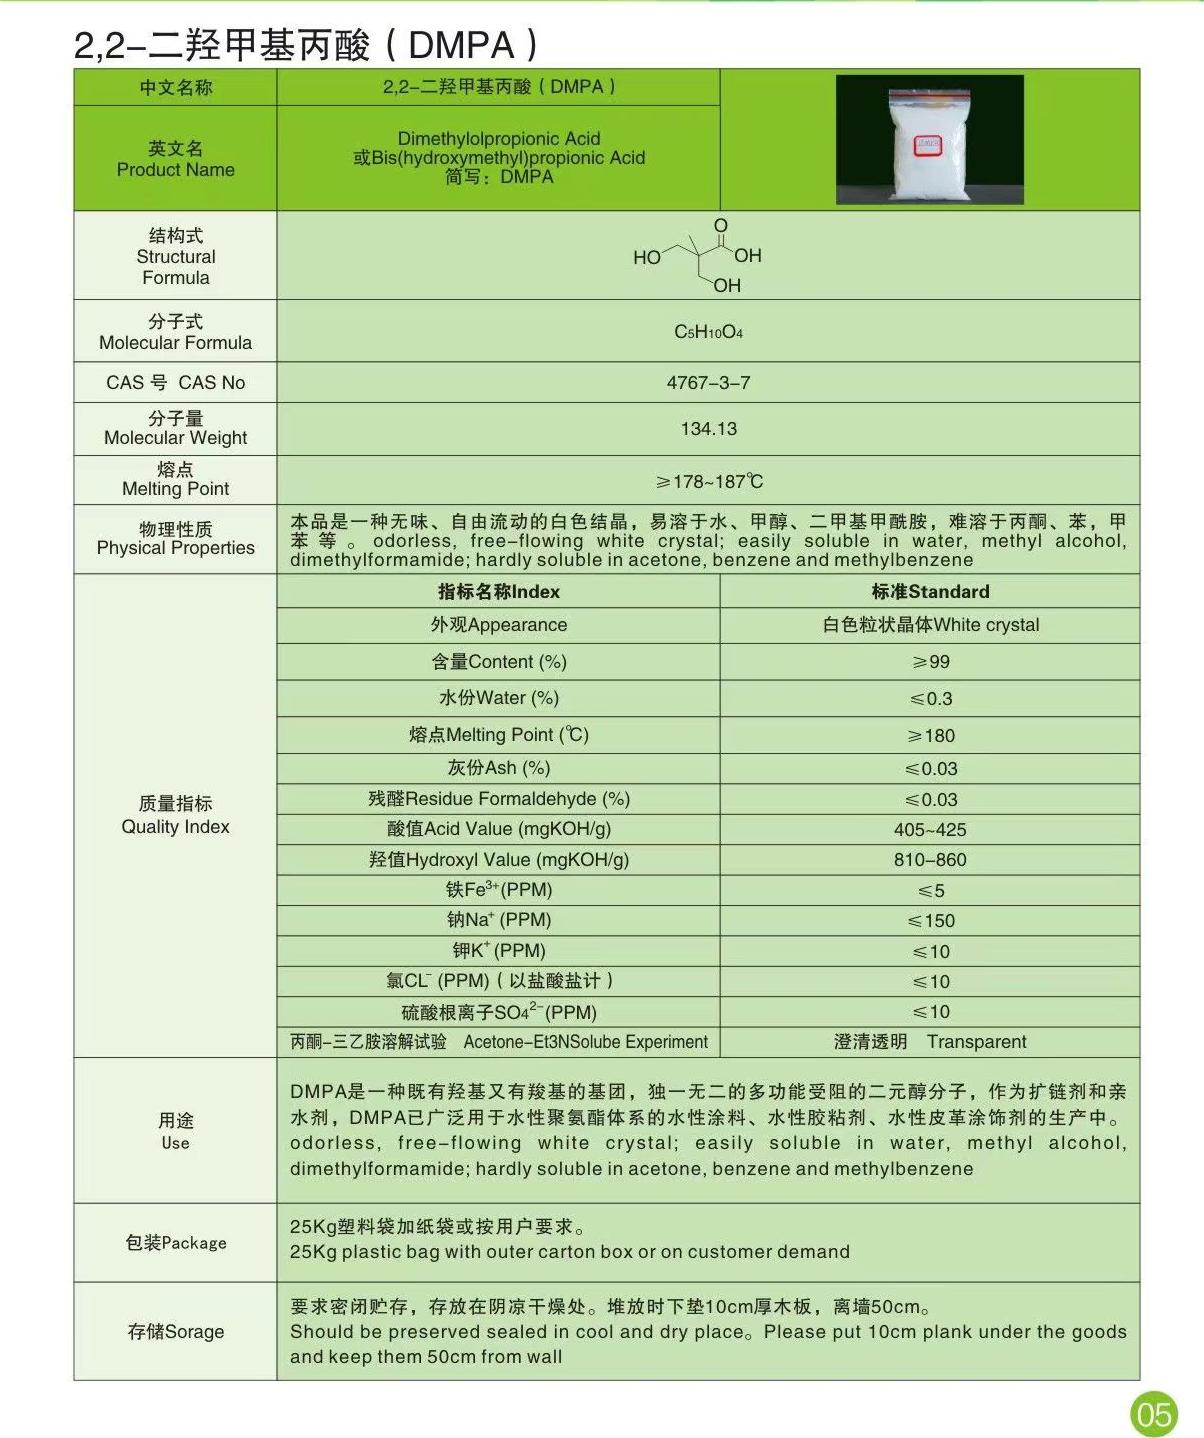
(DMPA) Market, Forecast, CAGR, Future Market Insights, Global Market, Growth, TrendsDimethylolpropionic Acid (DMPA) Market Set to Reach US$ 974.5 Million by 2033The global market for dimethylolpropionic acid (DMPA) is expected to grow at a CAGR of 6.4% during the forecast period from 2023 to 2033, according to a recent report by Future Market Insights, Inc. The report states that the current market for DMPA is worth US$ 524 million and is set to reach US$ 974.5 million by 2033, driven by the increasing demand for DMPA in various end-use applications.DMPA, also known as Bis-(hydroxymethyl) propionic acid, is a carboxylic acid that is widely used in the production of coatings, adhesives, and resins. It is a versatile chemical that offers excellent properties such as enhanced adhesion, flexibility, and durability to various products.Growth DriversThe DMPA market is expected to grow significantly during the forecast period due to several factors such as rising demand for eco-friendly coatings and adhesives, increasing investment in the construction industry, and growing demand for polyurethane and polyester resins.DMPA finds widespread applications in the production of paints and coatings. It helps in improving the properties of coatings such as scratch resistance, water resistance, weatherability, and adhesion. The global market for paints and coatings is growing due to increasing demand from the construction and automotive sectors, which is expected to drive the growth of the DMPA market in the coming years.DMPA is also widely used as a crosslinking agent in the production of adhesives, which are used in various industries such as automotive, construction, and packaging. The growing construction industry and increasing demand for flexible and durable adhesives are expected to drive the demand for DMPA in the adhesive industry.Regional AnalysisAsia Pacific is the largest market for DMPA, accounting for over 45% of the global market share. The region is expected to grow at the highest CAGR during the forecast period due to the increasing demand for coatings and adhesives in China and India. Additionally, the growth of the construction industry in the region is also driving the demand for DMPA.North America and Europe are also significant markets for DMPA, driven by the increasing demand for eco-friendly coatings and adhesives in the region. The regions are expected to grow at a moderate CAGR during the forecast period.Key PlayersThe key players in the global DMPA market include BASF SE, Evonik Industries AG, Tianjin Kaihong Chemical Co. Ltd., Zhejiang Wynca Chemical Industry Group Co. Ltd., GEO Specialty Chemicals, and Solvay SA.ConclusionThe global dimethylolpropionic acid (DMPA) market is set to grow significantly during the forecast period due to the increasing demand for eco-friendly coatings and adhesives, rising investment in the construction industry, and growing demand for polyurethane and polyester resins. The Asia Pacific region is expected to grow at the highest CAGR during the forecast period, driven by the increasing demand for coatings and adhesives in China and India. The key players in the market are BASF SE, Evonik Industries AG, and Solvay SA, among others.
Discover the Latest Advancements in Fabric Coatings
Title: Innovations in Fabric Coatings Open Doors to a World of Enhanced PerformanceIntroduction:In today's rapidly evolving market, fabric coatings play a vital role in enhancing the performance and functionality of textiles across various industries. With an increasing demand for durable, versatile, and sustainable solutions, innovative companies like {company name}, with their cutting-edge fabric coatings, are revolutionizing the textile industry. This article will delve into the advancements offered by {company name} and explore how these fabric coatings are reshaping various sectors, from fashion to automotive, and everything in between.1. Advanced Performance Fabric Coatings:{Company name}'s fabric coatings have been developed to enhance the properties of textiles, making them more durable, weather-resistant, and stain-resistant. By integrating advanced technologies, such as nanotechnology and polymer chemistry, the coatings are able to create a protective layer on the fabric surface without compromising its breathability or flexibility.These fabric coatings offer several advantages, such as increased resistance to water, oil, UV radiation, and flame retardancy. This makes them ideal for use in industries that require high-performance textiles, such as outdoor apparel, automotive upholstery, and protective gear for workers in hazardous environments.2. Sustainable Coating Solutions:In addition to their superior performance, {company name}'s fabric coatings are also eco-friendly and sustainable. The use of nanotechnology allows for reduced consumption of raw materials, energy, and water during the production process. Moreover, the coatings are designed to be free from harmful chemicals, making them safe for both users and the environment.By adopting sustainable coating solutions, {company name} is contributing to a greener future, aligning with the global efforts to reduce carbon footprint and promote sustainable practices in the textile industry.3. Fashion Industry Transformation:The fashion industry has greatly benefited from {company name}'s fabric coatings, as designers and manufacturers now have access to textiles with enhanced functionalities. The coatings allow for the creation of water-resistant, stain-resistant, and self-cleaning garments, ensuring durability and longevity. Additionally, the coatings can be applied to fabrics without altering their visual appearance or tactile properties. This versatility enables fashion designers to incorporate performance features into their creations without compromising on style or comfort.4. Automotive Advancements:Fabric coatings have also found applications in the automotive sector. {Company name}'s coatings can be applied to car seats, interior trimmings, and even convertible tops, offering protection against stains, spills, and fading caused by UV radiation. These coatings enhance the longevity and aesthetics of automotive interiors while providing easy maintenance and cleaning options. This, in turn, improves the overall driving experience and increases the resale value of vehicles.5. Medical and Protective Equipment:The medical and protective equipment industries have witnessed an increased demand for performance textiles in recent years. {Company name}'s fabric coatings offer anti-bacterial, anti-fungal, and anti-static properties, making them suitable for medical scrubs, surgical gowns, and protective gear.The coatings also provide resistance against fluid penetration, ensuring the safety and comfort of healthcare professionals. Furthermore, their high durability ensures that these textiles can withstand frequent washing and sterilization processes without compromising their effectiveness.Conclusion:With their advanced fabric coatings, {company name} is driving innovation across various industries, from fashion to automotive and medical equipment. These coatings offer improved functionalities, durability, and sustainability, allowing manufacturers and designers to create products that meet the evolving demands of consumers and businesses alike. As the textile industry continues to evolve, the importance of fabric coatings in enhancing performance and functionality will only continue to grow, and {company name} is leading the way in this transformative journey.
Waterborne Polyurethane: Applications, Benefits, and Market Trends
Certainly! Please provide the specific news content about Waterborne Polyurethane and the company introduction you would like me to use. Once I have those details, I will draft the 800-word news article for you.
Waterborne Polyurethane Resin: Key Features and Applications
Certainly! Please provide the news content about Waterborne Polyurethane Resin (with the brand name removed) and the company introduction you would like me to incorporate. Once I have those details, I can draft an 800-word news article for you.
Understanding the Meaning of Waterborne: Definition and Examples
Waterborne technology has been around for a while, but with the increasing focus on sustainability, its demand has significantly increased in recent years. This technology involves creating coatings or paints that can be applied to various surfaces and materials to make them water-resistant, replacing the traditional solvent-based coatings. The use of waterborne technology has significant environmental benefits as it reduces the emission of volatile organic compounds (VOCs) into the atmosphere.One of the leading companies in the development and production of high-performance waterborne coatings is {A}. With over 50 years of experience in this field, {A} has established itself as a reliable and innovative solutions provider.{A}’s waterborne coatings are designed to be highly durable while also being environmentally friendly. They offer a range of coating solutions for various industries, including automotive, industrial, aerospace, and marine. The coatings have been extensively tested and are known for their excellent adhesion, corrosion resistance, and weatherability.One of the key benefits of {A}’s waterborne coatings is their ability to reduce VOC emissions. VOCs are hazardous air pollutants that can have adverse effects on human health and the environment. Traditional solvent-based coatings release high levels of VOCs into the atmosphere during the application process. In contrast, waterborne coatings emit very low levels of VOCs, making them a more sustainable option.Another benefit of {A}’s waterborne coatings is their ease of application. They can be applied using conventional spraying equipment, making the transition from solvent-based coatings to waterborne coatings easy for manufacturers.{A}’s commitment to sustainability extends beyond its products to its operations. The company is actively working to reduce its carbon footprint and water usage. In 2020, {A} launched its “30 by 2030” initiative, which aims to reduce its greenhouse gas emissions by 30% by 2030.In conclusion, {A}’s waterborne coating technology offers a sustainable and durable alternative to traditional solvent-based coatings. Its commitment to sustainability and innovation has positioned it as a leader in the field. As more industries prioritize sustainability, the demand for waterborne coatings is likely to continue to grow, and {A} is well-positioned to meet that demand.